Choosing ready mix concrete can make a project more consistent, measurable, and efficient. The Global Cement and Concrete Association reports that the world uses approximately 14 billion cubic metres of concrete each year. This scale reflects concrete’s central role in housing, transport, energy, and commercial construction. It also explains why material control matters.
Ready mix concrete is produced in a controlled batching plant, then delivered to the site in rotating mixer trucks. This process can improve proportioning, moisture control, and placement speed. A project manager can order a specified strength, slump, and volume instead of mixing uncertain batches beside the foundation. Timing matters. A delayed truck can still create problems.
Dr. Karen Scrivener, a leading cement and concrete researcher, has said, “Concrete is the most used material in the world.” Her observation highlights both its value and its responsibility. According to the U.S. Geological Survey’s Mineral Commodity Summaries 2024, the United States shipped about 93 million metric tons of portland cement in 2023. That figure signals substantial construction demand, although cement consumption does not equal ready mix concrete production.
The practical advantage becomes visible on site: fewer raw-material piles, cleaner access routes, and a steady flow into formwork. Ready mix concrete can also reduce labor pressure and improve quality documentation. However, it is not automatically the best choice for every project. Small repairs, remote locations, or uncertain schedules may require another method. Specifications, weather, travel time, and supplier testing should be reviewed before ordering. Mistakes happen. Reliable decisions come from checking the details, not trusting the label alone.
Ready mix concrete is produced at a controlled plant and delivered to the jobsite in rotating trucks. It is not merely a delivery truck. Under ASTM C94/C94M, the concrete is specified, measured, mixed, transported, and discharged under defined requirements.
This supports consistent batching and clearer communication between the purchaser, producer, and testing team. It also helps reduce onsite material storage, hand mixing, and avoidable proportioning mistakes.
A common specification uses a 28-day compressive strength between 20 and 40 MPa. This value describes the required strength of properly cured concrete cylinders at 28 days.
It does not mean every batch reaches the same result automatically. Water added onsite, delayed discharge, poor consolidation, and inadequate curing can reduce performance. The testing laboratory should document sampling and test cylinders using recognized procedures, such as ASTM C39/C39M.
The project team should confirm strength, slump, air content, aggregate size, exposure conditions, and placement temperature before ordering. A 25 MPa mix may suit one slab but fail to meet another structure’s design or durability needs.
Delivery timing matters, too. Concrete that waits too long may lose workability before placement.
Small details matter here. I have seen specifications look complete while curing instructions remained vague. That gap deserves attention, because a strong mix cannot correct careless field handling.
Why Choose Ready Mix Concrete for Your Project?
Central batching gives concrete producers tighter control over water, cement, aggregates, and admixtures before delivery. Moisture probes can adjust batch water when sand arrives wetter than expected. Automated scales also reduce manual measuring errors. The result is more consistent slump from load to load.
ASTM C94/C94M provides clear slump tolerances. For a specified slump of 2 inches or less, the tolerance is ±1/2 inch. From over 2 to 4 inches, it is ±1 inch. From over 4 to 8 inches, it is ±1.5 inches. Above 8 inches, it is ±2 inches. ASTM C143/C143M defines the field slump test. Testing should occur at the proper discharge point, not after uncontrolled water addition. NRMCA’s Concrete in Practice No. 26 also identifies jobsite water addition as a major quality risk. More water may improve workability, but it can change strength and durability.
Tips: Confirm the target slump before batching. Record concrete temperature, arrival time, and discharge time. Check aggregate moisture data daily. Keep one sample for testing. No plant removes every variable. I have seen a good batch lose consistency after a long wait beside the formwork. That lesson is easy to forget. Crew communication still matters, even with accurate central batching.
| Control Dimension | Reference or Target | How Central Batching Supports Slump Control | Quality Benefit |
|---|---|---|---|
| Specified slump up to 2 in. (50 mm) or less | ASTM C94/C94M tolerance: approximately ±0.5 in. (±15 mm) | Accurate proportioning of water and aggregate moisture corrections helps keep the delivered slump close to the approved mixture target. | Reduces the risk of placing concrete that is too stiff for the intended application. |
| Specified slump above 2 to 4 in. (50 to 100 mm) | ASTM C94/C94M tolerance: approximately ±1 in. (±25 mm) | For a 4 in. (100 mm) target, an illustrative acceptance range is about 3 to 5 in. (75 to 125 mm), subject to the project specification and test conditions. | Provides a practical workability range for many slabs, footings, walls, and general structural placements. |
| Specified slump above 4 in. (100 mm) | ASTM C94/C94M tolerance: approximately ±1.5 in. (±40 mm) | Central batching can maintain the designed water-to-cementitious-material ratio while using approved admixture adjustments when high workability is required. | Supports placement in congested reinforcement and complex formwork without relying on uncontrolled water addition. |
| Aggregate moisture correction | Moisture is accounted for before water is added to the batch. | Batching calculations adjust the added water to reflect changing aggregate surface moisture and absorption. | Helps prevent unintended slump increases or decreases caused by wet or dry aggregates. |
| Water-to-cementitious-material ratio | Must remain within the approved mixture design and project specification. | Central batching records cementitious materials, batch water, aggregate moisture, and approved liquid admixtures for each load. | Improves consistency while protecting specified strength, durability, and shrinkage requirements. |
| Slump test method | ASTM C143/C143M | A representative sample is tested using a standardized slump cone procedure at the required sampling location. | Creates a consistent basis for comparing measured workability with the specified slump. |
| Concrete sampling | ASTM C172/C172M | Sampling procedures are used to obtain material representative of the delivered load rather than relying on a single unrepresentative portion. | Improves confidence that the test result reflects the concrete being placed. |
| Water or admixture adjustment at delivery | Only permitted when allowed by the approved mixture design, specification, and ASTM C94/C94M requirements. | Any authorized addition is measured, documented, and followed by sufficient mixing before acceptance testing. | Maintains traceability and reduces uncontrolled changes to workability and performance. |
| Batch and delivery records | Load-specific documentation should identify mixture proportions, batch quantities, added water, admixtures, and relevant times. | Electronic or printed batch records allow production personnel and project teams to review consistency from load to load. | Supports quality control, troubleshooting, acceptance decisions, and project documentation. |
Choosing ready mix concrete can make project costs easier to control. A typical truck carries about 6–10 m³, so one delivery can cover a large slab or footing. This scale reduces repeated small-batch mixing on site. It also limits idle time between pours. On a busy morning, that difference is practical. Fewer mixing tasks mean fewer labor hours. Crew members can place, vibrate, and finish concrete instead.
Material waste also falls when quantities are calculated from drawings and measured areas. A site team can order close to the required volume, allowing a small allowance for uneven ground and spillage. Excess concrete is expensive and difficult to handle. I have seen a poorly measured pour leave several wheelbarrows unused. That was not a dramatic failure, but it exposed weak planning. Ready mix does not remove every cost risk. Delays, difficult access, or a slow pump can still raise labor expenses. Confirm truck access, discharge time, and required strength with the project engineer or concrete technician.
Tips: Measure length, width, and depth twice. Add only a sensible allowance. Group pours when possible to use truck capacity efficiently. Keep the route clear before delivery. Record actual used volume after finishing. This simple record improves the next estimate.
Quality verification starts before the truck reaches the site. Under ASTM C172/C172M, technicians sample concrete from the middle portion of discharge. They avoid the first and last flow. Slump, temperature, air content, batch time, and cylinder numbers need clear records. These details connect a test result to an actual placement. ASTM C39/C39M governs compressive strength testing of molded cylinders. A perfect cylinder is rare. A tilted specimen or damaged end can distort reported strength.
The 28-day age usually comes from project specifications or structural codes. ASTM C39 itself explains the test method, not every acceptance requirement. The cylinder remains properly cured before entering a calibrated compression machine. A 6-by-12-inch cylinder failing at 100,000 pounds produces approximately 3,540 psi. The calculation is simple; interpretation is harder. One result does not represent every cubic yard.
ACI 318-19 generally requires the average of three consecutive strength tests to meet the specified strength. For concrete rated at 5,000 psi or less, no individual test may fall more than 500 psi below that value. NRMCA guidance also stresses representative sampling, curing, and technician training. Field work can still be imperfect. Labels smear, curing boxes lose water, and busy crews rush sampling. Better practice uses duplicate records, protected cylinders, and immediate communication when seven-day results trend downward. A 28-day number needs context.
Ready mix concrete offers controlled batching, documented proportions, and predictable delivery. ASTM C94/C94M generally requires concrete discharge within 90 minutes after water contacts cement. It also limits drum mixing to 300 revolutions, unless project specifications allow different conditions. These limits protect workability and reduce avoidable quality variation.
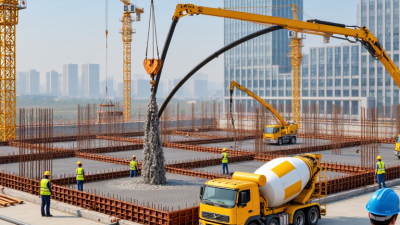
On site, timing becomes physical and visible. A truck arrives, the pump line is primed, and crews begin placing concrete near the forms. Delays can cause slump loss, cold joints, or difficult consolidation. ASTM C94/C94M allows adjustments when agreed by the purchaser and producer. However, added water can change performance. It should never become a casual fix. NRMCA guidance on ordering ready mixed concrete also stresses clear delivery information, including required slump, strength, volume, and placement conditions.
Tips: Confirm the batch time before discharge. Keep the access road clear. Prepare enough workers and vibration equipment. Record any water or admixture additions. Check the concrete temperature and slump when required.
The 90-minute limit is helpful, but it is not magic. Weather, traffic, drum speed, and placement rate still matter. A practical team watches the load, not only the clock. That detail is easy to miss. A documented delivery ticket also supports traceability when results require review.